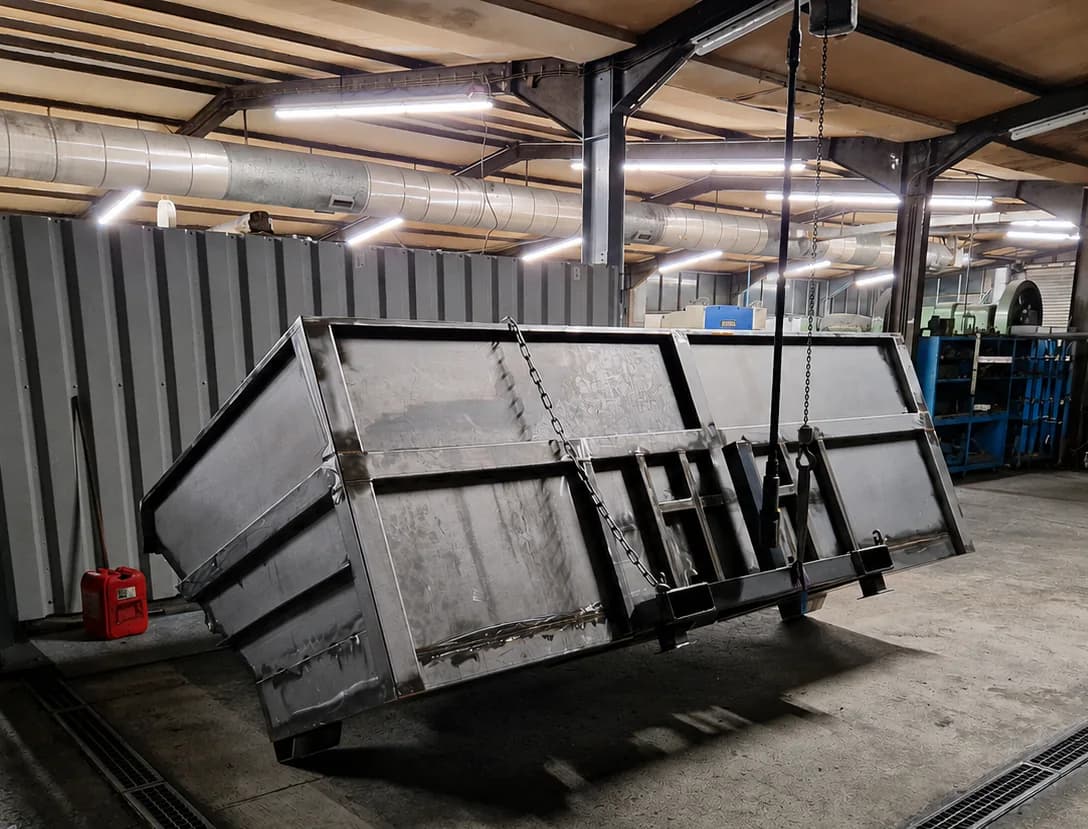
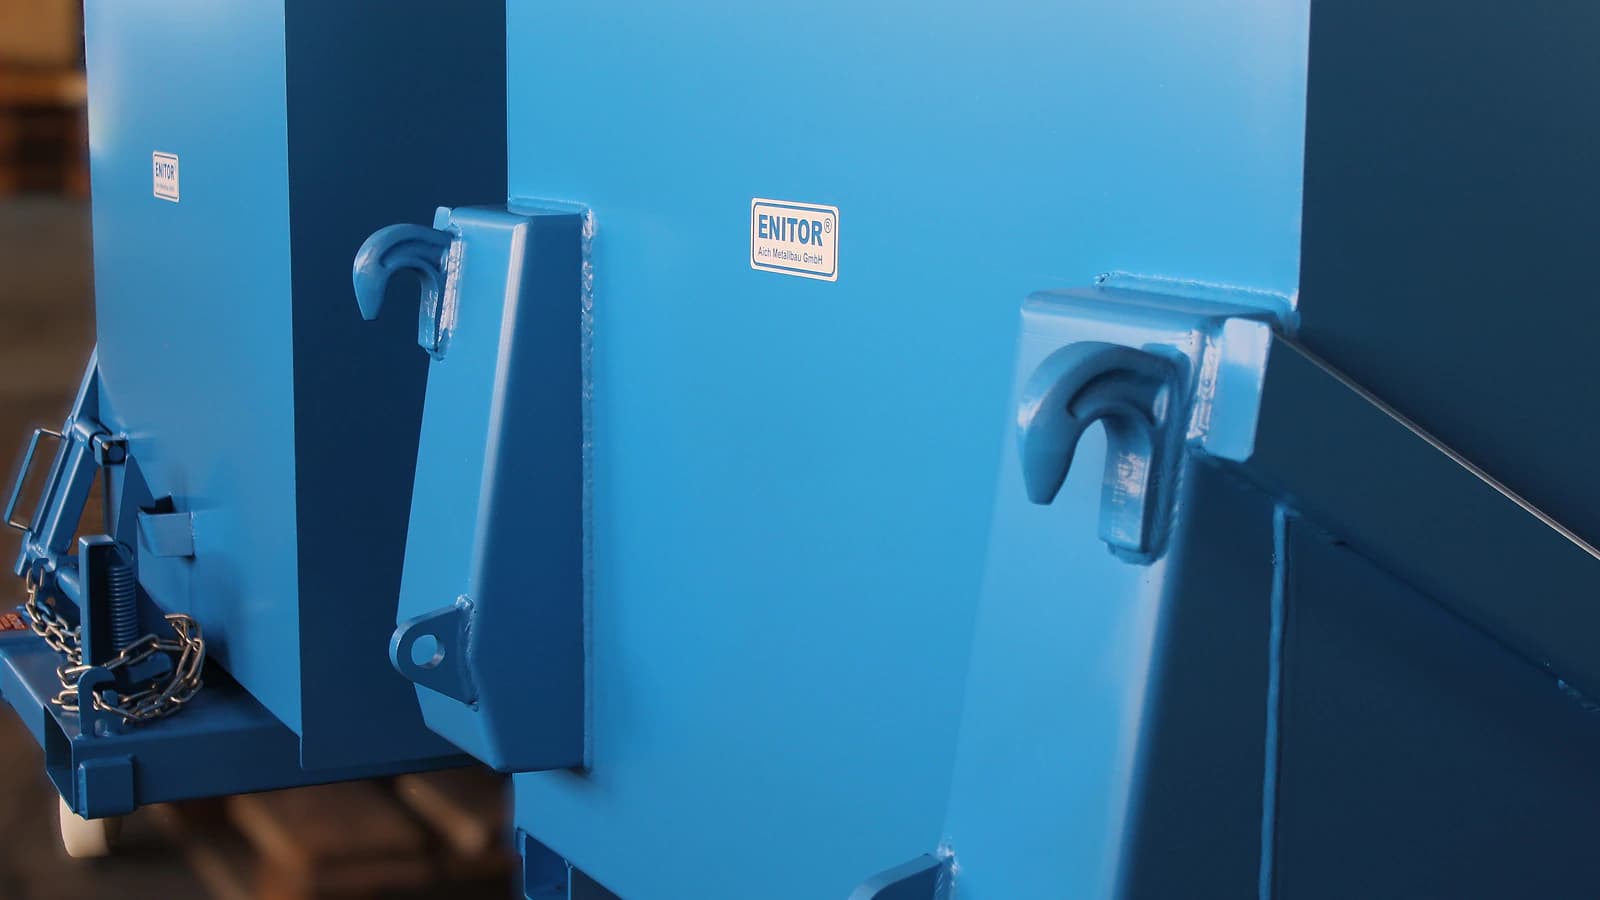
Short paths support technical clarification and practical adjustments during the project.
ENITORPROCESS 01—04
01 / 04
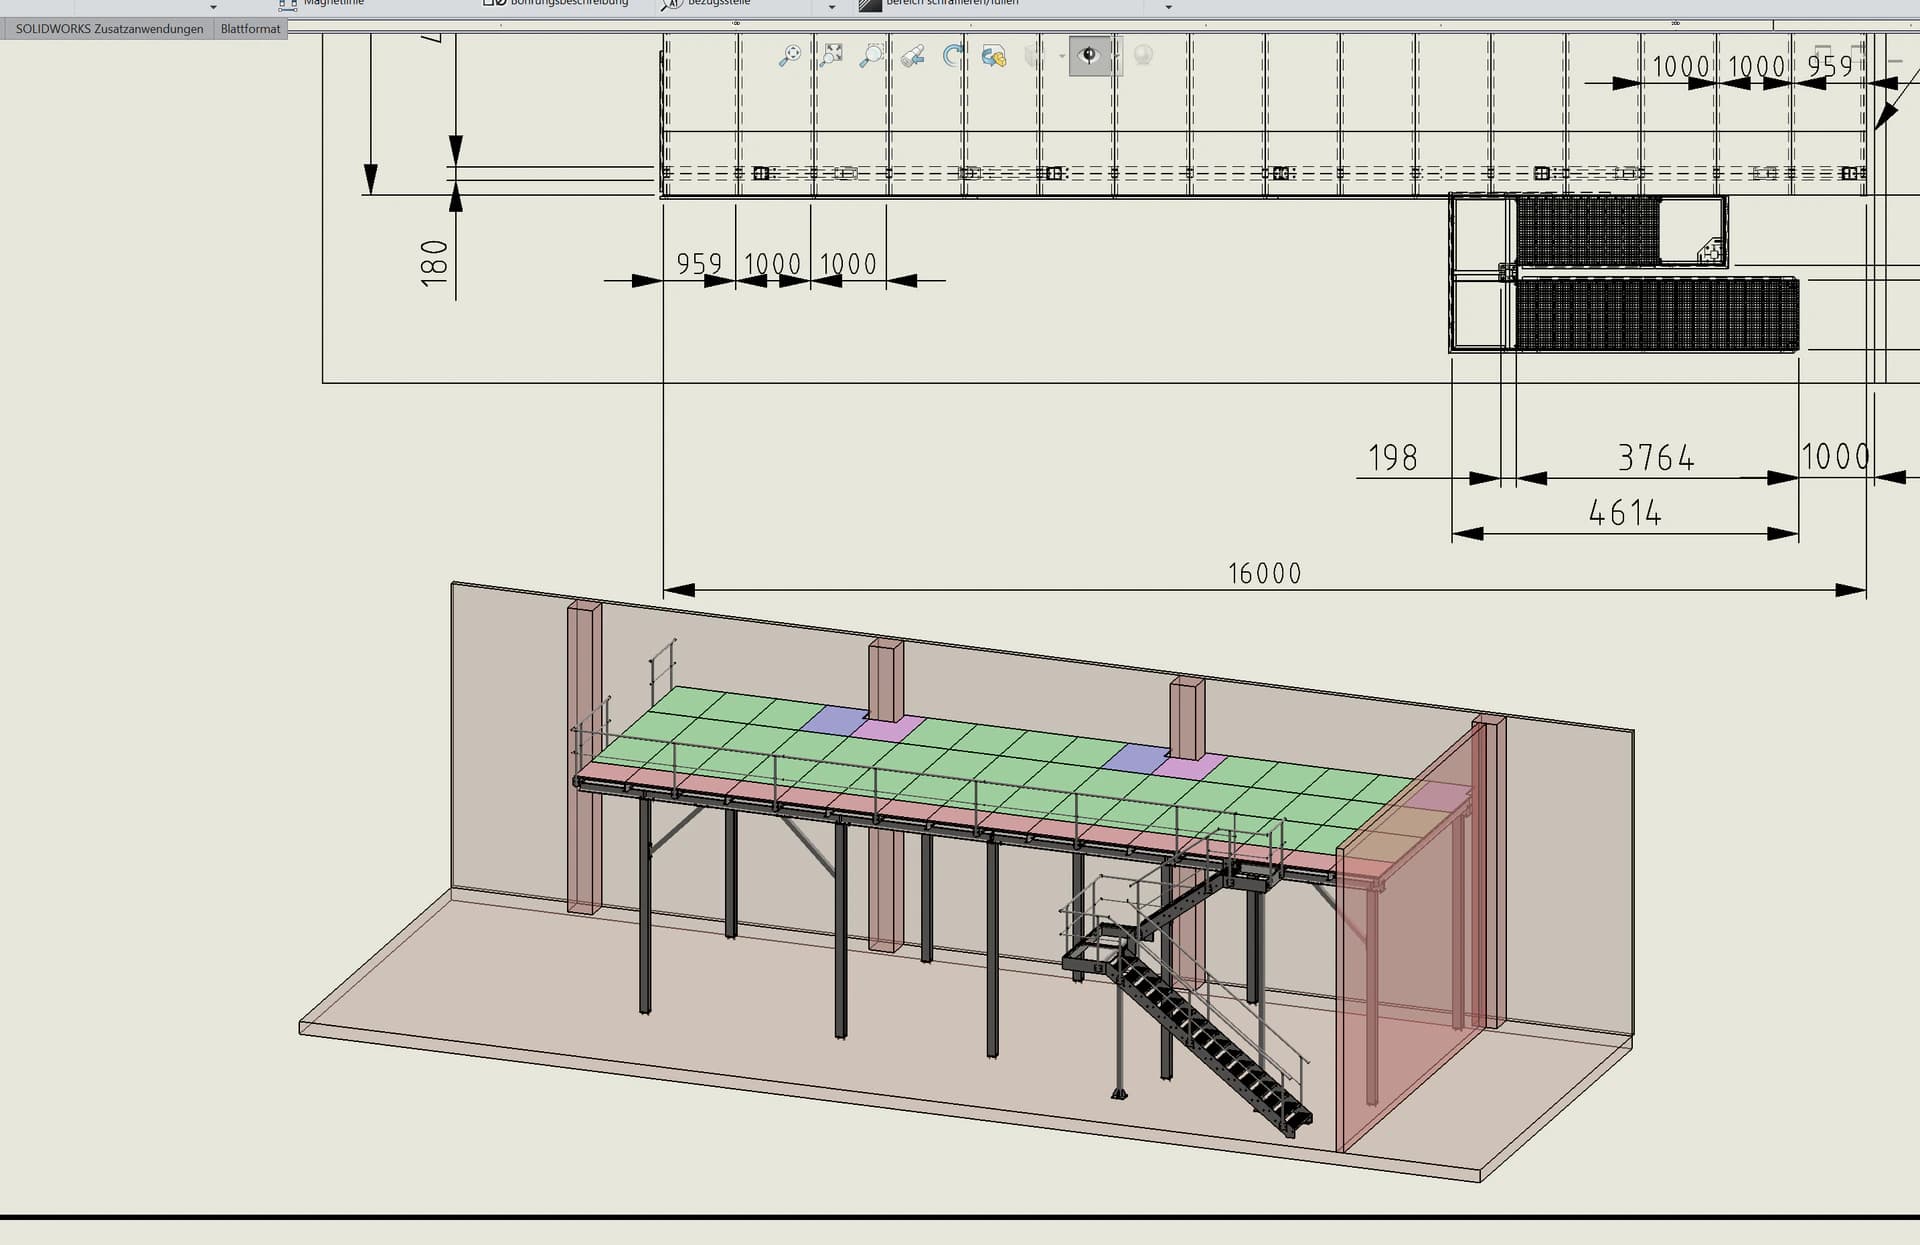
SolidWorks engineering
Requirements and interfaces are transferred into an agreed manufacturing model.
02 / 04
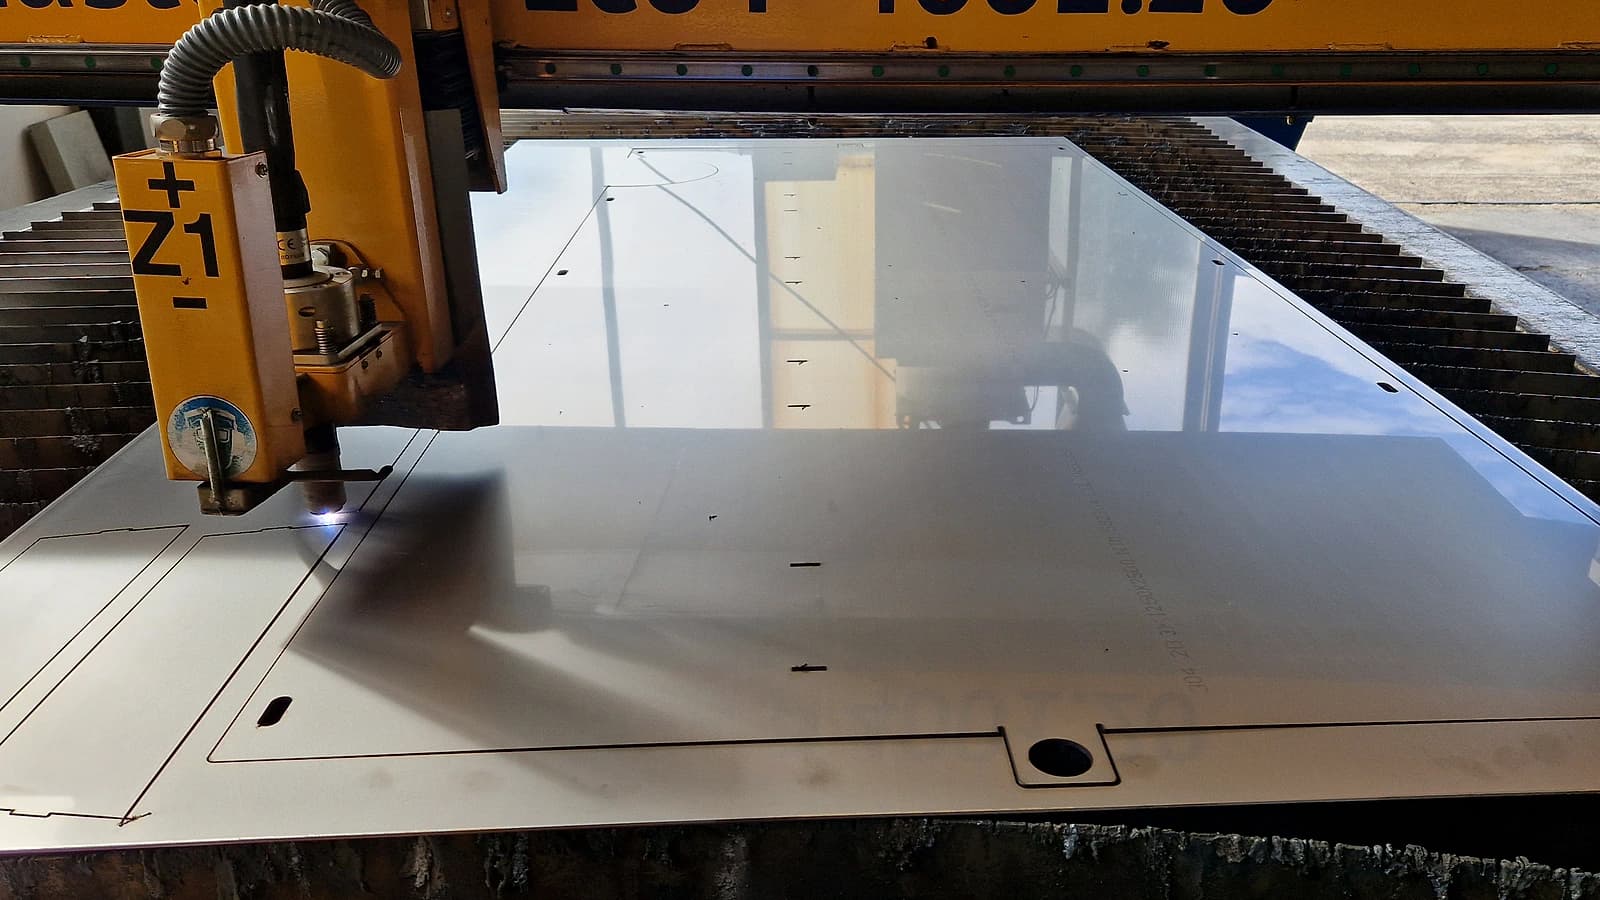
Workshop manufacturing
Components are cut in the workshop and prepared for further manufacturing.
03 / 04
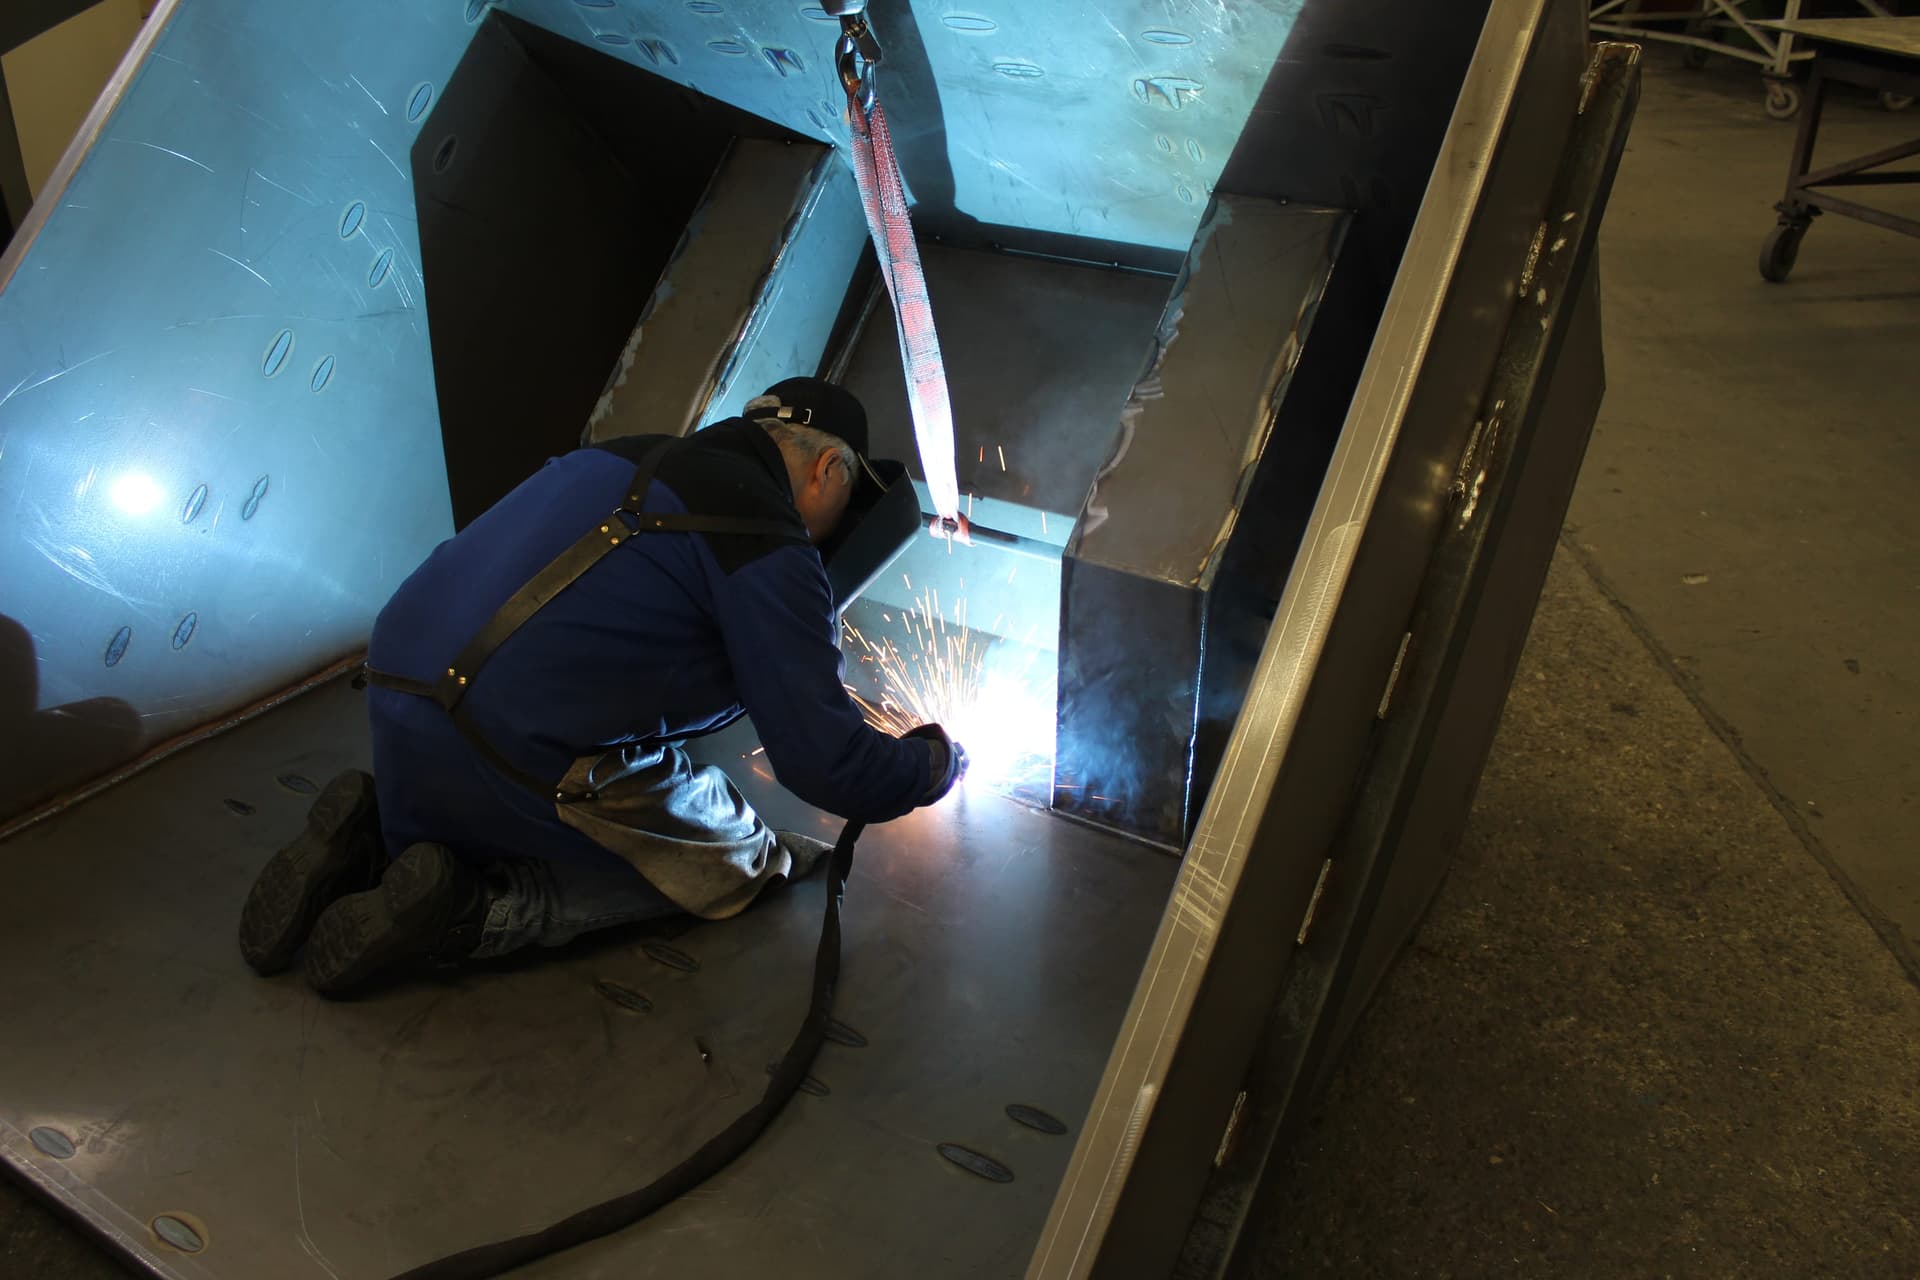
Welded structures
Steel parts are joined into project-specific assemblies.
04 / 04
Painting and finish
Manufactured components receive the agreed paint finish.
In-house manufacturing depth
From sheet cutting to the painted product.
With its versatile machinery, ENITOR manufactures individual containers, assemblies and structures. The essential processing steps are brought together at the Munderkingen site.
Munderkingen production site
One location links the essential manufacturing stages.
ENITOR manufactures individual containers, assemblies and structures with a versatile range of machinery. Cutting, forming, mechanical processing, grinding, welding and painting are coordinated as one process chain at the Munderkingen site.
Because the component remains close to the people responsible for the next step, technical questions and practical adjustments can be resolved through short communication paths.
Direct process control
Quality, dimensional accuracy and execution remain visible.
Around 90% in-house manufacturing means that ENITOR produces most of the components and individual parts required for its products itself. This reduces dependencies on external suppliers and keeps the decisive processing stages within the company.
The high level of vertical integration gives ENITOR direct influence over quality, dimensional accuracy and execution. At the same time, the sequence can be adapted flexibly when individual customer requirements call for changes.
The process chain
How material becomes a finished product.
Each stage prepares the component for the next. The result is a traceable route from material preparation through forming and assembly to the final surface finish.
Cutting
Prepare and cut the material
At the start of the process chain, sheet, round and profile material is prepared to suit the component. The guillotine shear cuts sheet metal up to 8 mm thick quickly and accurately. Individual contours are produced on the CNC plasma cutting system – in quality cutting for S235 steel up to 15 mm and for stainless steel and aluminium up to 10 mm each. Circular and band saws complete the cutting options for profiles, round material and other workpieces.
Forming
Machine, form and press brake
After cutting, pillar and radial drilling machines provide drilling and further mechanical processing directly at the site. Only at the end does the 160-tonne press brake form the sheet metal precisely into the intended shape, creating accurately fitting bends for containers and structures.
Joining
Prepare surfaces, weld and assemble
Before joining, edges and surfaces are prepared as required using a range of grinding and processing tools. ENITOR then selects the welding equipment and process to suit the material, component and requirement. This creates durable joints and robust assemblies for structures and containers.
Finishing
Paint and finish
Manufactured components and containers can be coated directly afterwards in the in-house paint booth. They receive the agreed surface finish and, depending on the coating, additional protection from external influences. This keeps the chain closely coordinated from the first sheet to the fully processed and painted product.
Machinery and capabilities
The individual operations at a glance.
Guillotine shear
Sheet metal up to 8 mm thick is cut quickly and accurately in preparation for the next manufacturing steps.
Sheet metal up to 8 mm
CNC plasma cutting
Individual contours and complex geometries are produced under CNC control with precision and repeatability.
S235 steel up to 15 mm
Stainless steel up to 10 mm
Aluminium up to 10 mm
Circular and band saws
Round and profile material, along with other workpieces, is cut cleanly to size using the appropriate sawing process.
Round and profile material
Press braking
The 160-tonne press brake forms sheet metal into accurately fitting components for structures and containers.
160-tonne press force
Drilling and machining
Pillar and radial drilling machines enable flexible drilling and further machining steps directly in the workshop.
Pillar and radial drilling machines
Grinding and surfaces
Edges and surfaces are finished as required and prepared for the subsequent manufacturing steps.
Edge and surface finishing
Welding
Welding equipment and processes are selected to suit the material, component and requirements for durable joints.
For structures and containers
Painting
In the in-house paint booth, components and containers receive their agreed surface finish and coating directly after manufacturing.
In-house paint booth
For our customers, this means short communication paths, fast response times, close quality control and flexible solutions for individual requirements.
ENITOR / MUNDERKINGEN
Manufactured where engineering can ask directly.
The workshop image shows manufactured products and the manufacturing environment at the Munderkingen site.
Inside the workshop
Manufacturing in Munderkingen. Products made in-house.
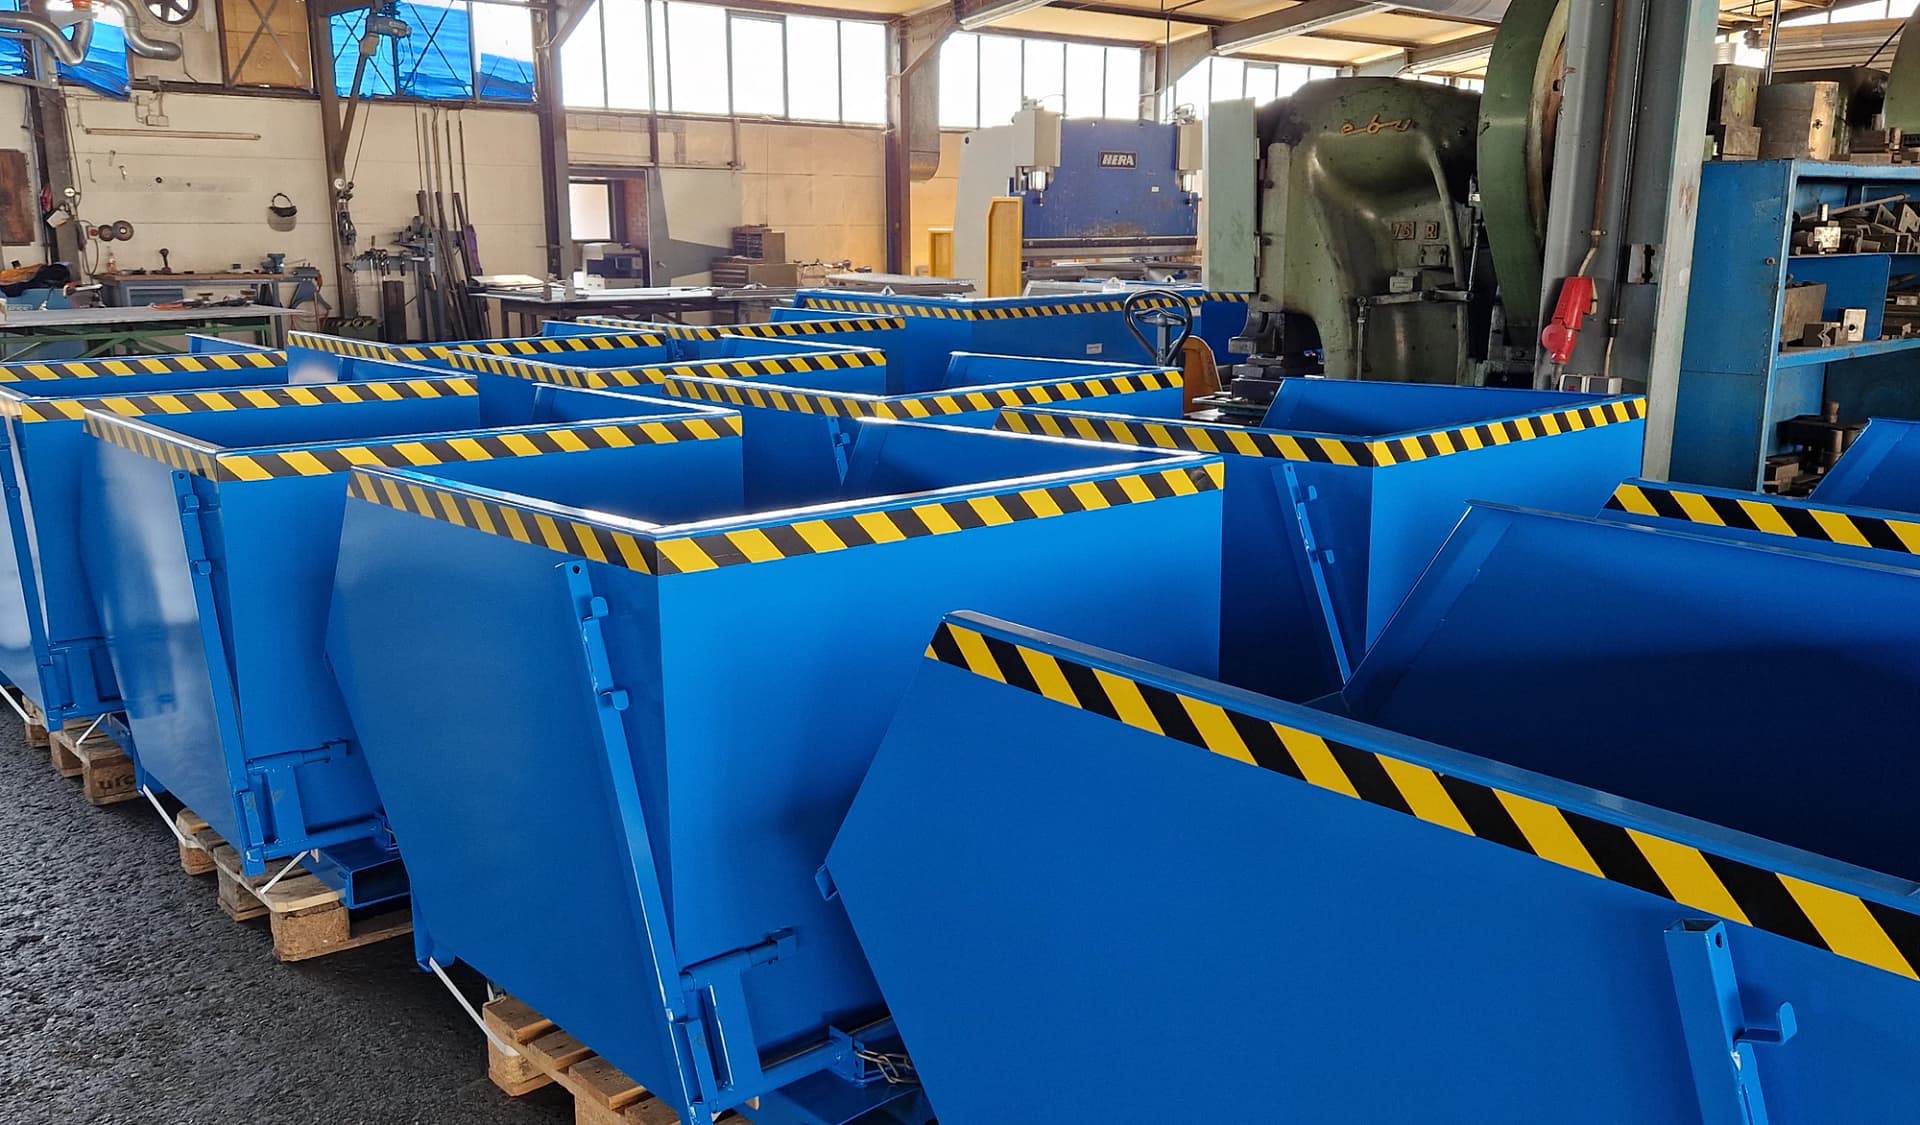
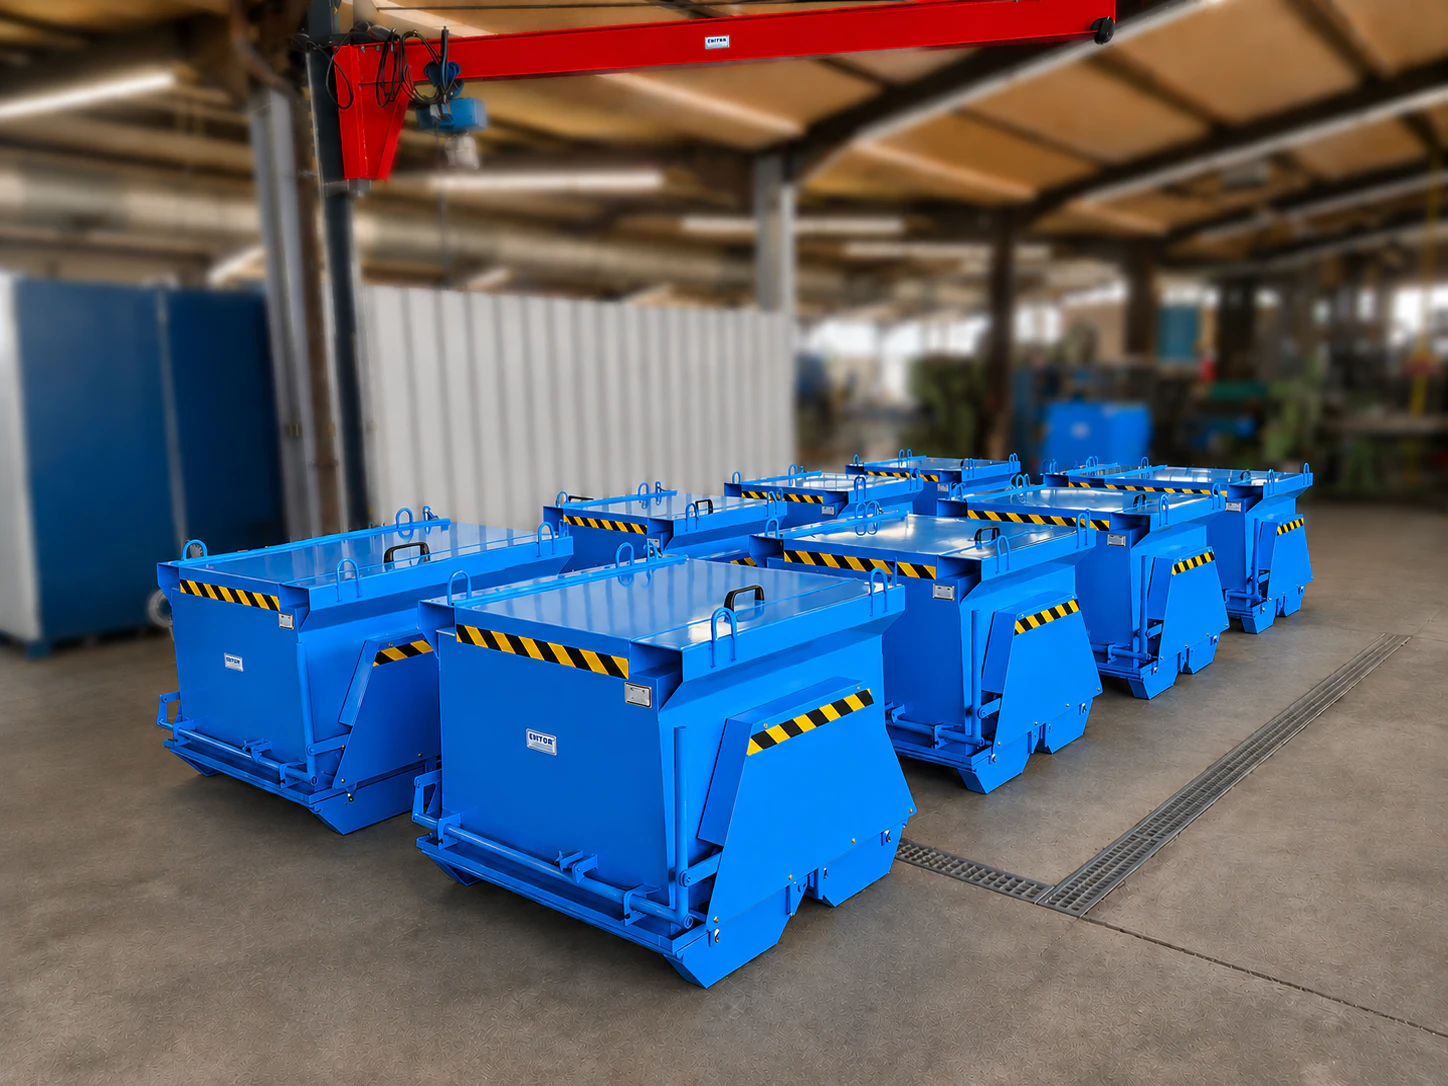
Current views from our workshop show series production, material flow and the machinery at the Munderkingen site.
Series production
Finished containers before delivery
Material flow
Container systems straight from the workshop
Workshop machinery
Manufacturing and final assembly at one site
Manufacturing quality
Details that make the execution visible.
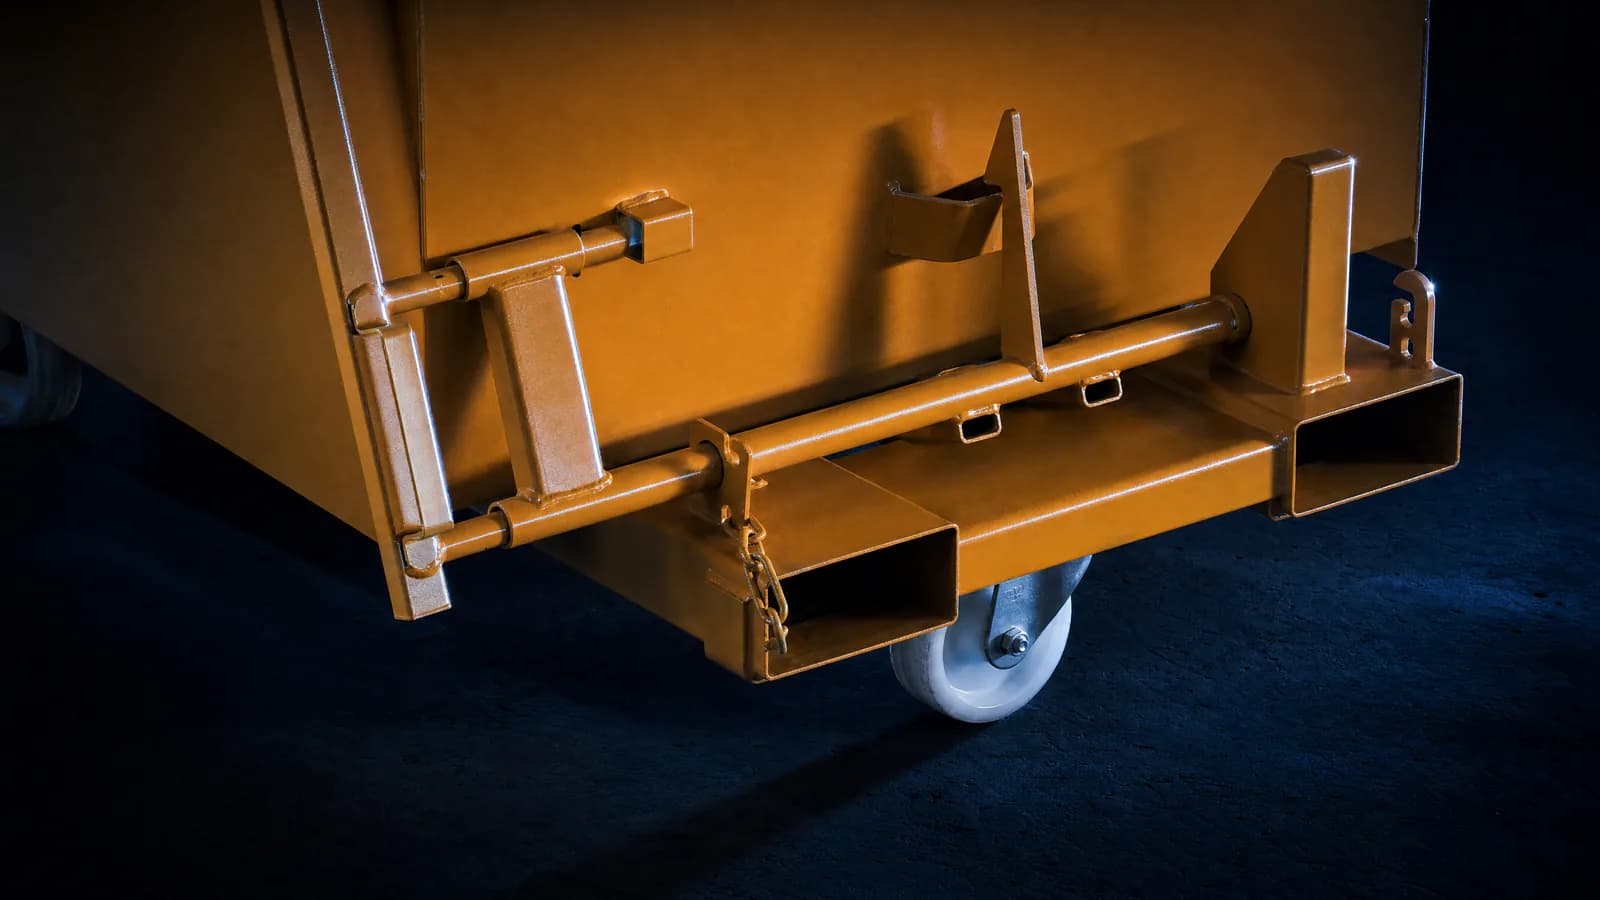
Tipping mechanism in detail
Bearings, release linkage and fork pockets as a traceable technical assembly.
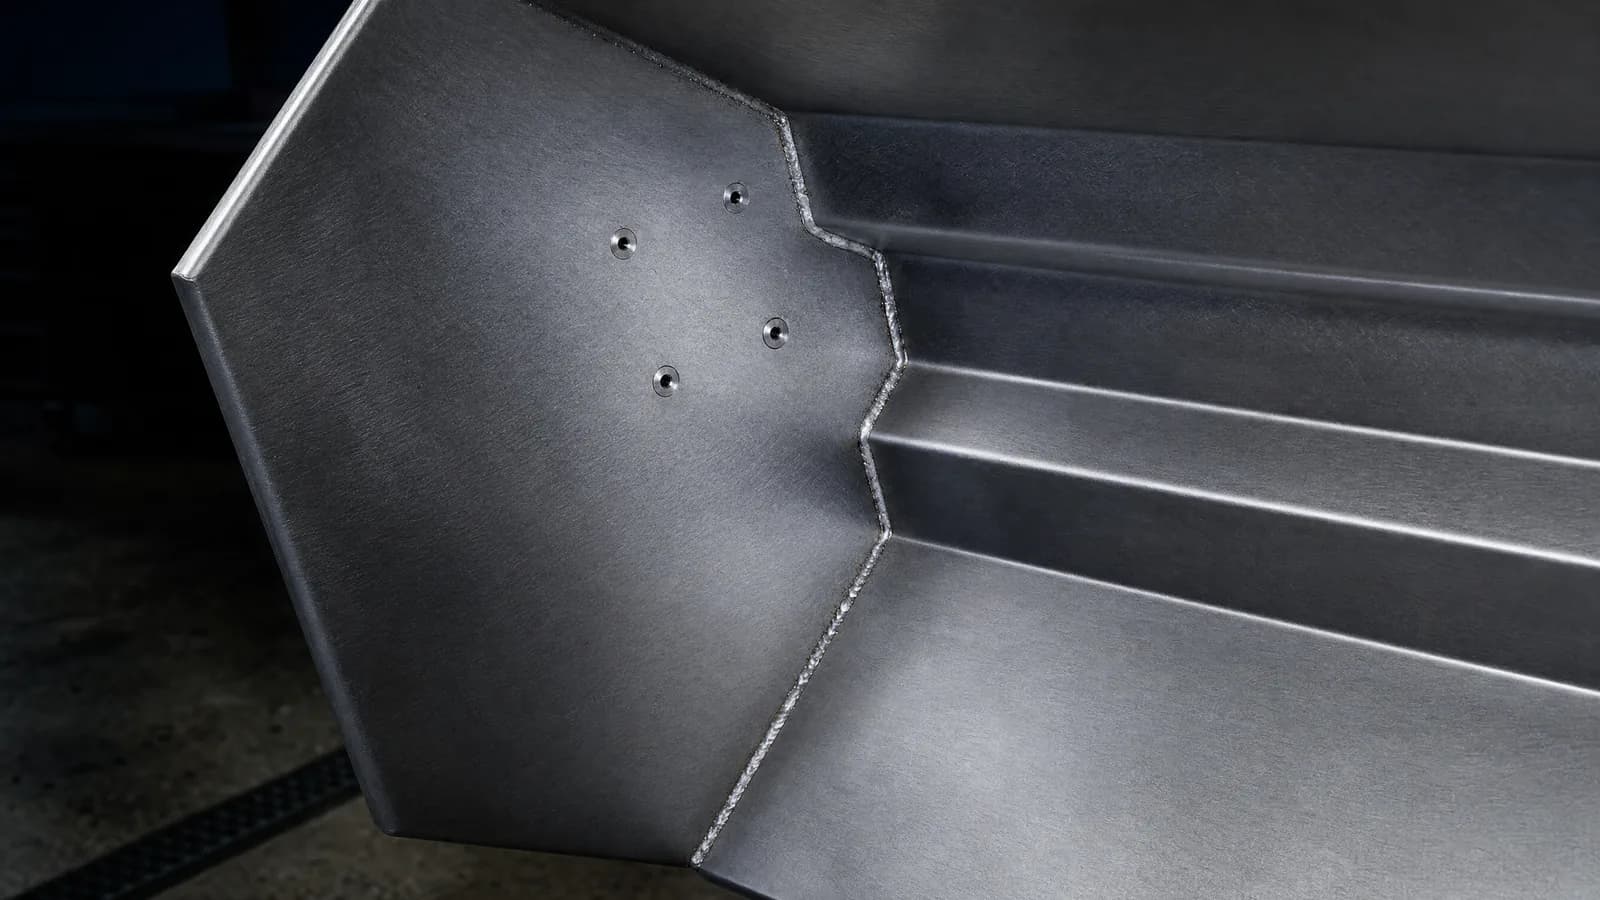
Weld seam and sheet transition
Contour, seam path and material surface in a close technical view.
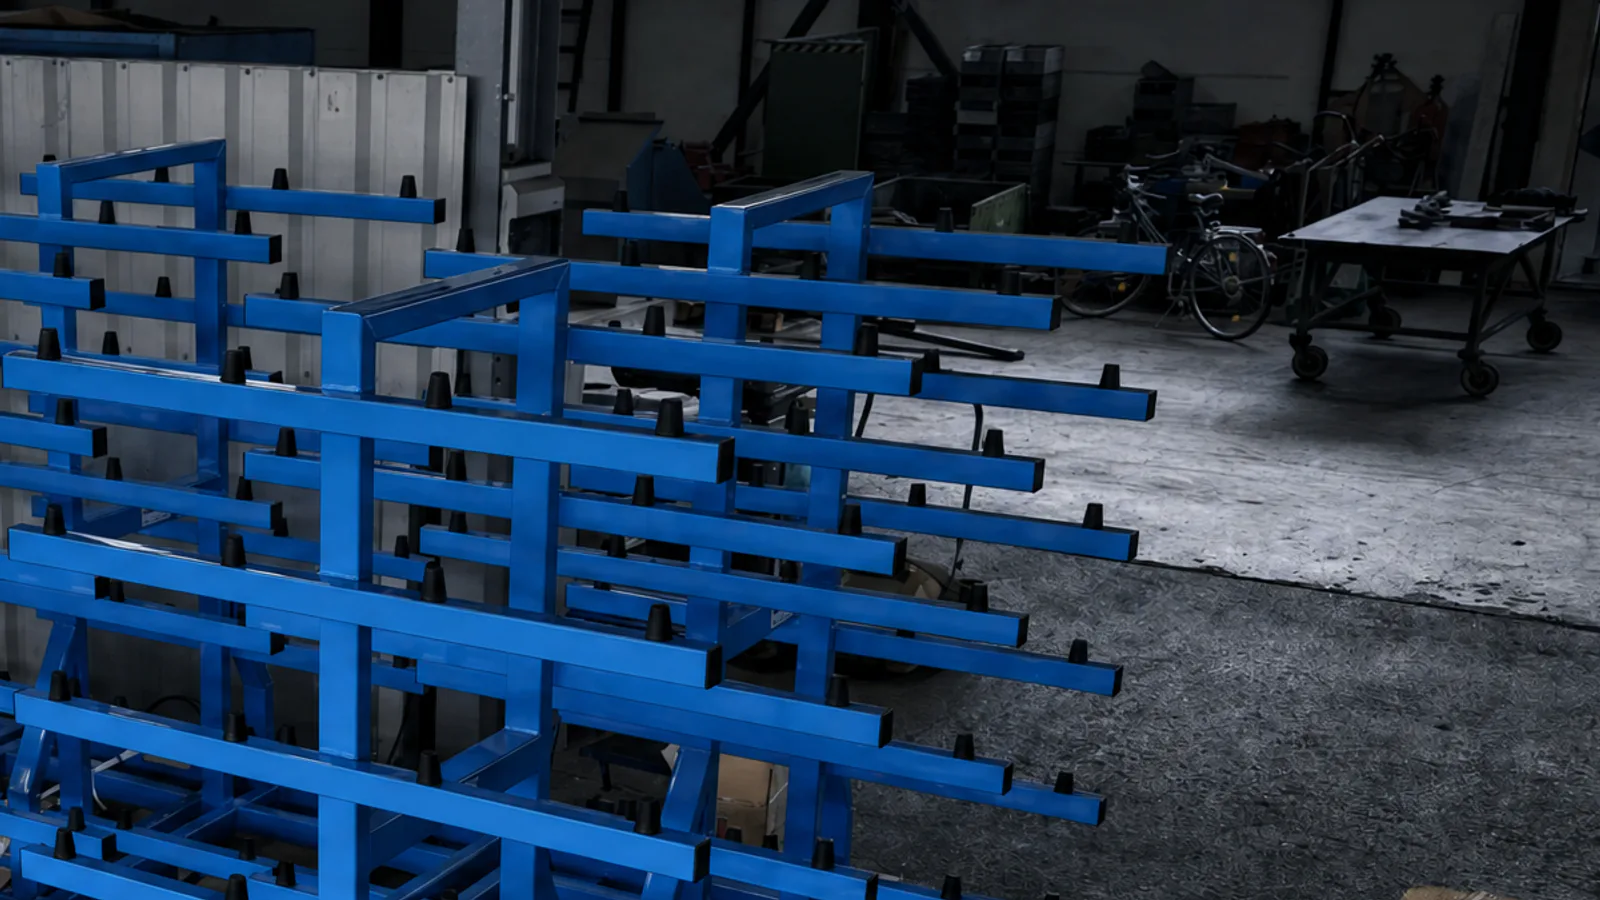
Welded rack joint
Profile connections and repeatable joining points from a real rack series.
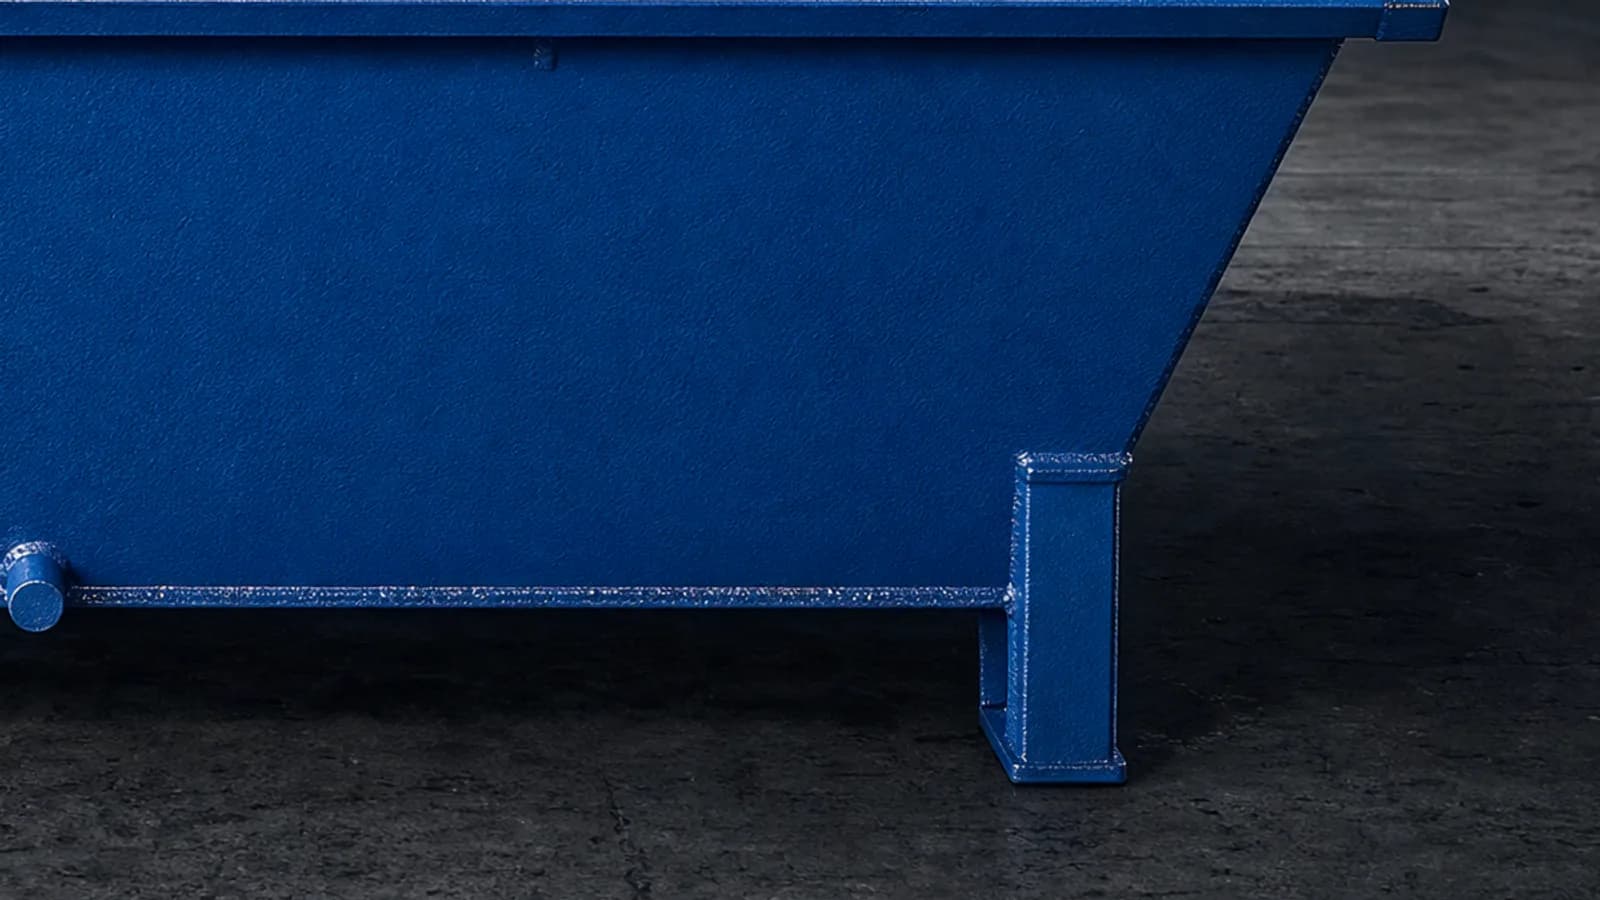
Support foot and container edge
Support surface, edge geometry and weld execution of a manufactured custom container.
Project flow
From clarification to handover.
Clarify
Capture the application, environment, interfaces and objective.
Engineer
Develop the solution and approval status in SolidWorks.
Manufacture
Produce components and assemblies from the agreed design.
Inspect
Inspect the execution and agreed requirements on the actual component.
Deliver
Coordinate documents, delivery and next steps.
Would you like to discuss manufacturability?
Send the task and available technical files to ENITOR.